Business Details
43 Years
experience
Your Trusted Source for High-Barrier Metallized Films
Celplast Metallized Products Metallized Products has been a trusted leader in the metallized film industry since 1983. Our patented Metacoat technology revolutionized barrier performance, offering up to 10 times improvement over conventional films. We specialize in high-barrier metallized and clear films for the converting industry, serving diverse markets including food packaging, pharmaceuticals, and industrial applications. Our commitment to innovation is matched by our dedication to sustainability, providing recyclable and compostable solutions that meet evolving environmental standards. With over 40 years of experience, we combine technical expertise with a customer-centric approach to deliver tailored packaging solutions.Our state-of-the-art facilities and self-directed work teams ensure precision and accountability in every project. We pride ourselves on being the industry's preferred partner for metallizing services and custom film development. Our global reach extends through regional representatives across North America, Asia, Mexico, and Central America. Backed by numerous industry awards, we continue to set benchmarks in barrier film technology. Our culture of continuous improvement drives us to exceed customer expectations in quality, service, and innovation.
Services
High-barrier films
Metallized packaging
Sustainable solutions
Contract metallizing
Transparent barrier films
Details
- Year established: 1983
Highlights and features
- We offer 40+ years of specialized expertise in metallized film technology
- Our patented Metacoat inline topcoat system delivers 10x barrier improvement
- We provide fully recyclable and compostable packaging solutions
- Our toll metallizing services handle webs up to 100 inches wide
- We maintain ISO-certified quality control processes
Services
High-Barrier Films
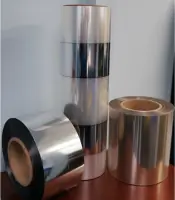
Our high-barrier metallized films provide superior oxygen and moisture protection for extended product shelf life. Using patented Metacoat technology, these films deliver 10x improved barrier performance compared to conventional options. Ideal for food packaging, pharmaceuticals, and industrial applications requiring critical protection.
Sustainable Packaging
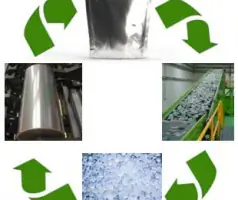
We develop recyclable and compostable packaging solutions using metallized polyethylene and PLA films. Our products enable mono-material structures that meet How2Recycle standards while maintaining high barrier properties. This includes PCR-content films and AlOx-coated transparent options for environmental compliance.
Contract Metallizing
Our toll metallizing services handle webs up to 100 inches wide with precision top-coating capabilities. We offer custom metallization patterns and controlled-density deposition for microwave packaging applications. Complete traceability is maintained through our comprehensive lab services and quality control processes.
Transparent Barrier Films
These high-clarity films combine laboratory-grade barrier performance with product visibility. Using vacuum-applied AlOx coatings on various substrates, they provide oxygen, moisture, and aroma protection without obscuring product presentation. Available in mono-material recyclable configurations for multiple industries.
Reflective Insulation
Our low-emissivity metallized films offer corrosion-resistant thermal protection for insulation and cold chain applications. REFLECT-MET products provide temperature resistance up to 500F with emissivity values as low as 0.05, suitable for building insulation, protective packaging, and industrial applications requiring radiant barrier properties.
People
Dante Ferrari
President
Leading Celplast Metallized Products Metallized Products's strategic direction, Dante Ferrari brings extensive industry experience to drive innovation in metallized film technology. His leadership focuses on sustainable solutions and global market expansion while maintaining technical excellence.
Chuck Larsen
Co-Founder
As co-founder, Chuck Larsen established Celplast Metallized Products Metallized Products's metallizing expertise in 1983. He pioneered early innovations that positioned the company as North America's preferred contract metallizer for polypropylene film manufacturers during its formative years.
Bill Hellings
Co-Founder
Co-founder Bill Hellings contributed to Celplast Metallized Products Metallized Products's transformation into a high-value barrier product provider during the 2000s. His vision helped develop certified metallized film solutions that expanded the company's market reach across multiple industries.
Questions
What makes your metallized films different from traditional foil packaging?
Our metallized films offer superior flexibility and weight advantages over foil while maintaining equivalent barrier properties. They provide better shelf appeal, improved supply chain reliability, and recyclable options that traditional foil cannot match.
How do your sustainable packaging solutions maintain barrier performance?
We use patented Metacoat technology and AlOx coatings to create recyclable mono-material structures that preserve oxygen, moisture, and aroma protection without compromising environmental credentials.
What customization options are available for metallized films?
We offer stripe metallizing patterns, controlled-density deposition for microwave applications, and substrate-specific coatings on polyester, polypropylene, PLA, and PE materials to meet unique packaging requirements.
What industries benefit most from your barrier film solutions?
Our films serve food packaging (dry/powder/liquid), pharmaceuticals, industrial applications, and consumer goods sectors requiring extended shelf life and product protection in demanding environments.
How do you ensure quality in your metallizing process?
We maintain rigorous quality control through in-line monitoring, comprehensive lab testing, and ISO-certified processes that guarantee consistent metal adhesion, barrier performance, and product specifications.
What support do you provide for custom packaging development?
Our technical team offers full application support, including substrate selection, barrier requirement analysis, and process optimization to create tailored solutions that meet specific packaging challenges and sustainability goals.