Business Details
50+ Years
experience
Leading Manufacturer of Commercial Refrigeration Equipment
KeepRite Refrigeration has been a trusted leader in commercial refrigeration since 1945, delivering innovative solutions for food storage, industrial cooling, and pharmaceutical applications. Our expertise spans the design, engineering, and manufacturing of evaporator coils, condensing units, and heat recovery systems, supported by state-of-the-art facilities in Brantford, Ontario, and Longview, Texas. With over 80 years of global experience, we prioritize quality through our ISO 9001-certified processes, ensuring reliable performance and customer satisfaction.Our commitment to continuous improvement drives advancements in energy efficiency and sustainability, exemplified by technologies like SMARTSPEED and ESP+. Backed by a nationwide network of sales offices and dedicated support, we empower refrigeration professionals with cutting-edge tools, comprehensive warranties, and personalized service to meet specialized industry needs.
Services
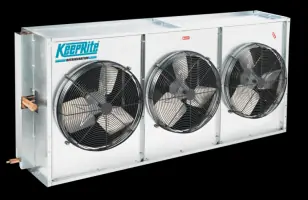
Evaporators
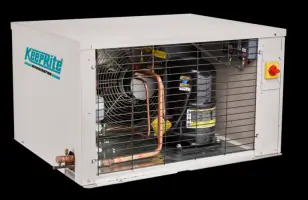
Condensing Units
Multi-Compressor Systems
Heat Reclaim Systems
Fluid Coolers
Coils
Air Handlers
Details
- Year established: 1945
Highlights and features
- We offer over 80 years of expertise in commercial refrigeration design and manufacturing.
- Our ISO 9001-certified quality management ensures consistent, reliable product performance.
- Advanced technologies like SMARTSPEED and ESP+ deliver superior energy efficiency.
- Nationwide sales and support network provides localized, responsive service.
- Comprehensive design tools and technical resources empower refrigeration professionals.
Associations and certifications
- ISO 9001:2015
Services
Evaporators
Our evaporators provide precision cooling for food storage, industrial processes, and pharmaceutical applications. Engineered for efficiency and durability, these systems ensure optimal temperature control while minimizing energy consumption. Customizable configurations meet specialized requirements across commercial refrigeration sectors.
Condensing Units
High-performance condensing units designed for reliability in demanding environments. Featuring QUIETUNIT technology and A2L refrigerant compatibility, these systems combine energy efficiency with reduced sound levels. Available in hermetic, scroll, and semi-hermetic models for diverse industrial applications.
Heat Reclaim Systems
ThermoSaver heat reclaim systems capture and repurpose waste heat for water heating or space heating. This sustainable solution reduces energy costs while maintaining refrigeration efficiency. Ideal for supermarkets and industrial facilities seeking eco-friendly operational improvements.
Parallel Compressor Systems
Modular parallel compressor systems optimize cooling capacity and energy use in large-scale operations. Designed for flexibility, these systems allow seamless expansion and efficient load management. Suitable for supermarkets, cold storage warehouses, and industrial processing plants.
Fluid Coolers
Direct-drive fluid coolers deliver efficient heat rejection for industrial process cooling applications. Engineered for durability in harsh environments, these systems maintain consistent performance while reducing maintenance requirements. Available in medium and large capacity models.
Questions
What types of refrigeration products does KeepRite offer?
We provide evaporators, condensing units, heat reclaim systems, parallel compressor systems, fluid coolers, and air handlers for commercial and industrial applications.
Are your products energy-efficient?
Yes, our SMARTSPEED, ESP+, and QUIETUNIT technologies optimize energy use while maintaining performance.
Do you offer support for refrigeration professionals?
We provide design tools, technical documentation, parts locators, and live support Monday-Friday 8 AM-7 PM EST.
Where are your manufacturing facilities located?
We operate facilities in Brantford, Ontario, and Longview, Texas, with nationwide sales offices across North America.
Are your products ISO certified?
Yes, our quality management system is ISO 9001:2015 certified for design, manufacturing, and delivery processes.
What industries do you serve?
We support food processing, supermarket refrigeration, pharmaceuticals, and industrial process cooling applications.
Videos